Product Overview
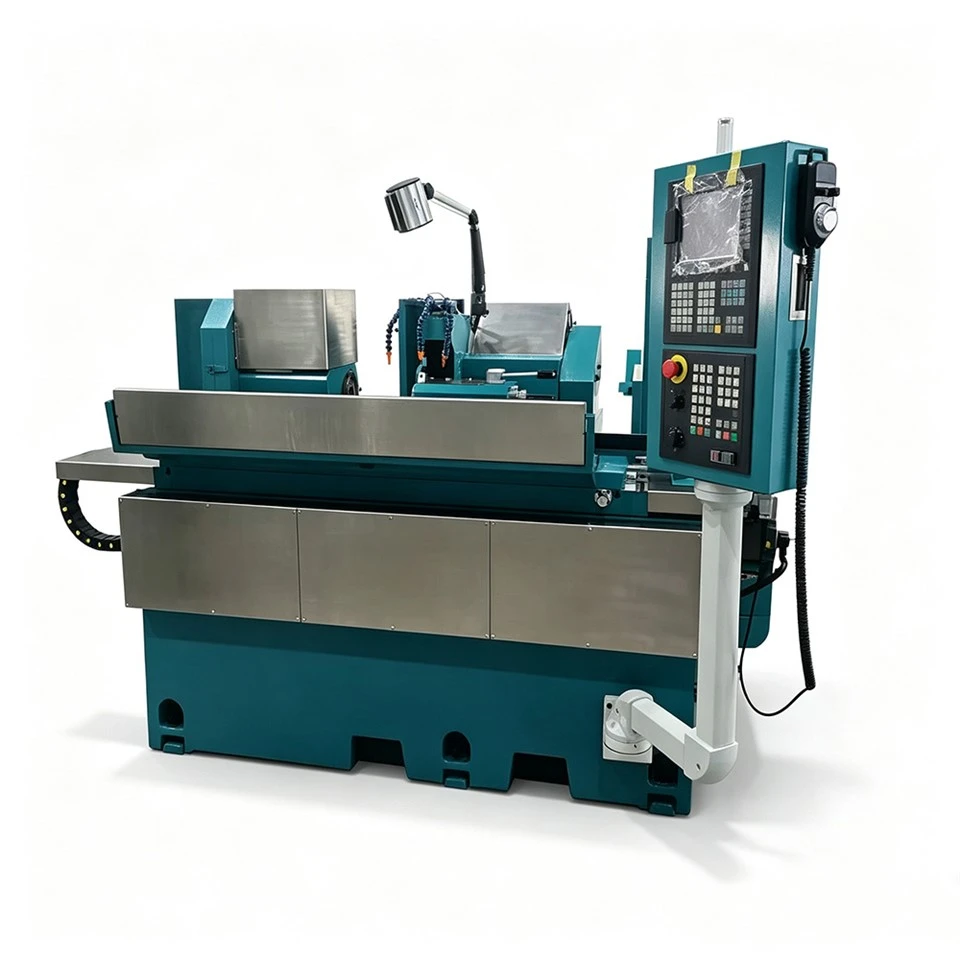
This CNC cylindrical grinding machine is engineered for high-precision external diameter, step, and tapered face grinding on rotational components. Built on a cast Meehanite iron bed with finite element analysis (FEA) optimization, the machine structure absorbs high cutting forces while maintaining thermal equilibrium. Linear axes (X and Z) are driven by closed-loop AC servo motors coupled directly to precision preloaded ball screws, achieving a positioning accuracy of 0.001 mm and a repeatability of 0.0005 mm.
-
![CNC Cylindrical Grinder]() CNC Cylindrical Grindercnc or not:CNC voltage:380 V, 220 V grinding diameter(outer)(mm):320 grinding diameter(inner)(mm):125 max. length of workpiece (mm):1000view more
-
![Normal Cylindrical Grinding Machine]() Normal Cylindrical Grinding MachineCNC cylindrical grinding machine for internal and external grinding, MachineMachine table longitudinal travel, wheel head raped approach and withdrawal and automatic periodic cross infeed are...view more
-
![Punch Grinder Machine]() Punch Grinder MachineClamping working diameter:Φ3.0-50mmview more
Spindle speed:0-20000rpm
Processing inner hole diameter:Φ1.0-40mm
Work head rotation speed:0-180rpm
Grinding accuracy... -
![High Precision Synchronous Cylindrical Grinder]() High Precision Synchronous Cylindrical GrinderHigh precision, high rigidity, and high efficiency are the key characters of this grinder, reaching the perfect combination of outstanding performance and high efficiency. Can be widely used in...view more
-
![CNC Cylindrical Grinding Machine]() CNC Cylindrical Grinding MachineMinor customizationview more
Drawing-based customization
Sample-based customization
Full customization -
![New Cylindrical Grinding Machine]() New Cylindrical Grinding MachineM Universal cylindrical grinder seriesview more
Custom OEM Solutions Available -
![Heavy Duty Cylindrical Grinding Machine]() Heavy Duty Cylindrical Grinding MachineHeavy Duty Cylindrical Grinding Machineview more
High Precision Cylindrical Grinding Machine
Maximum swiveling diameter:φ240 / φ350
Distance between Centers:520mm / 765mm /...


Key Features
Hydrodynamic Wheel Spindle
Supported by multi-point hydrodynamic oil film bearings, isolating the grinding wheel from vibration and maintaining a radial runout below 0.001 mm.
B-Axis Wheelhead Swivel
Programmable B-axis positioning enables automated angular transitions for multi-diameter stepped shafts without manual fixture adjustments.
Integrated Acoustic Emission (AE) Sensor
Detects initial wheel-to-workpiece contact and monitors dress intervals in real-time, reducing idle cycle times by up to 18%.
Full Enclosure Coolant Management
External chiller units regulate coolant temperature within +/- 0.5 degrees C of ambient workspace temperature to prevent thermal expansion of the workpiece.
Machining Capabilities
Dimensional Tolerance
IT5 to IT6 cylindrical accuracy.
Surface Finish
Achievable roughness down to Ra 0.2 um (material dependent).
Workpiece Capacity
Maximum swing diameter 320 mm to 500 mm; distance between centers from 1000 mm to 2000 mm.
Max Workpiece Weight
Up to 150 kg between centers.
Machine Configuration
CNC System
FANUC 0i-TF Plus or Siemens Sinumerik 828D with conversational grinding cycles.
Drive Motors
Fanuc absolute encoder servo motors on X and Z axes.
Workhead
Variable speed spindle driven by an AC inverter (10 to 500 RPM).
Tailstock
Hydraulic quill actuation with adjustable thrust force to prevent workpiece distortion.
Application
Automotive
Transmission shafts, camshafts, CV joint components, and rotor shafts.
Aerospace
Landing gear struts, hydraulic actuators, and turbine shafts.
Industrial Power
Electric motor rotors, precision ball screws, and hydraulic pump spools.
Determine Workpiece Geometry: Match maximum length and swing diameter requirements against table travel limits and center height.
Evaluate Material Removal Rate (MRR): Select wheel spindle power (7.5 kW to 18.5 kW) based on stock allowance and hardness of hardened alloy steels (HRC 55-65).
Define Automation Level: Choose between manual loading for low-volume toolrooms or gantry loader / robotic integration for continuous cell production.
Manufacturing & Quality Control
Bed Casting Aging
Meehanite iron castings undergo thermal annealing and natural seasoning for 90 days to eliminate internal residual stress prior to precision guideway grinding.
Laser Interferometer Calibration
Every machine axis is laser-calibrated for pitch, yaw, and linear displacement errors to conform to ISO 230-2 standards.
Ballbar Testing
Circular interpolation tests are executed on X and Z axes to verify contouring accuracy and eliminate servo mismatch.
72-Hour Burn-in Test
Continuous dry-run testing under simulated load conditions validates thermal stability and hydraulic circuit integrity before crating.
Optional Configuration
In-Process Gauging
Marposs or Renishaw measuring heads for automatic size control without retracting the wheel.
High-Speed CBN Wheel Package
Wheel peripheral speed up to 80 m/s with dedicated high-pressure coolant filtration system (10 bar).
Automatic Balancing System
Dynamic balancing head on the wheel spindle to neutralize vibration from wheel wear during heavy stock removal.
FAQ
As one of the most professional cylindrical grinding machine manufacturers in China, we're featured by quality products and good price. Please rest assured to buy high-grade cylindrical grinding machine for sale here from our factory. If you have any enquiry about cooperation, please feel free to email us.
Cylindrical Grinder with Ball Screw, Cylindrical Shaft Grinding Machine, Precision Grinding Machine for Workshop